Material removal
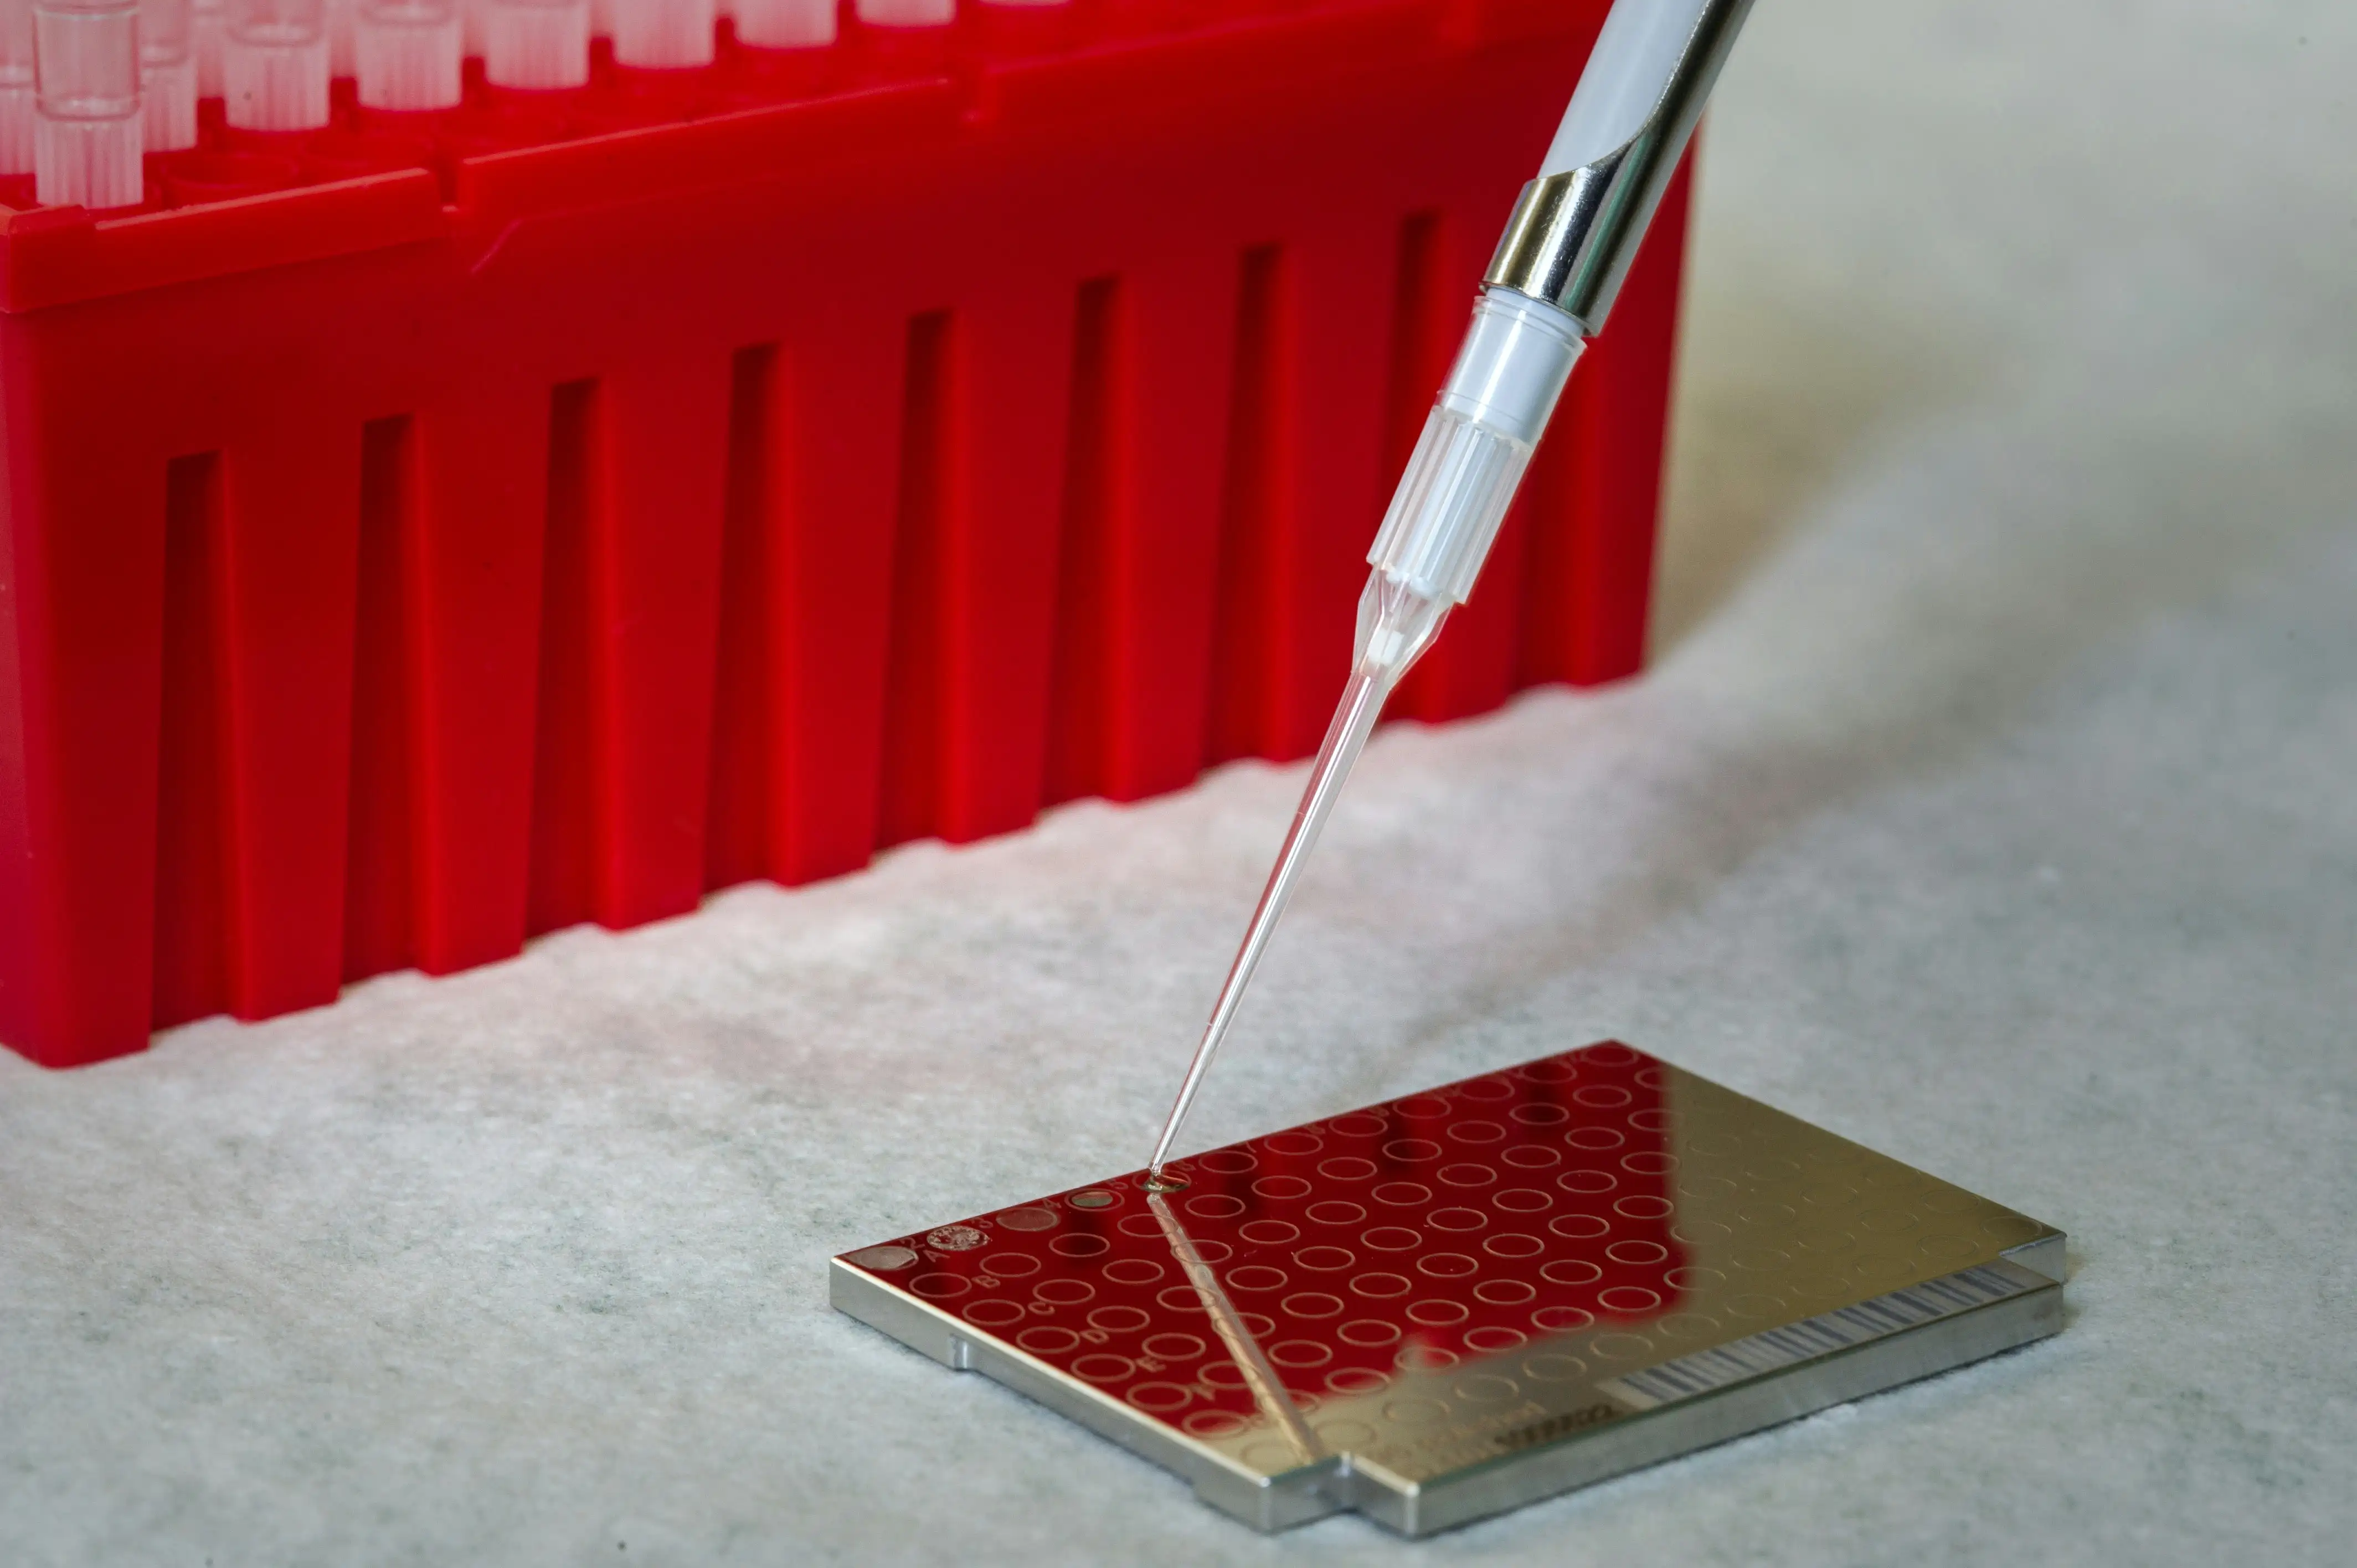
Select laser, punch, waterjet, or etching around thickness, edge quality, and volume.

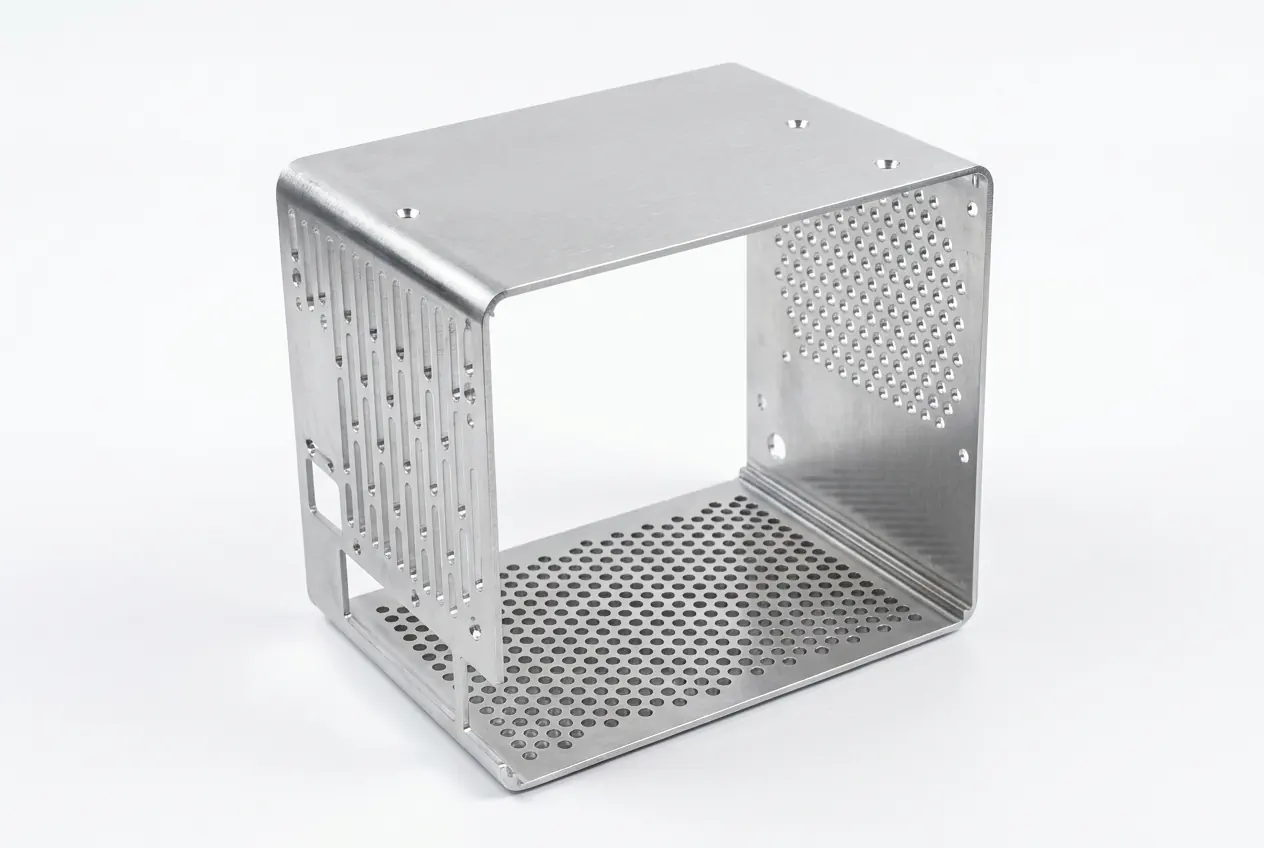
Turn your CAD files into custom sheet metal prototypes and small production batches. ZigiTech makes enclosures, brackets, and chassis with laser cutting, bending, welding, and finishing for product testing and end-use parts.


For a prototype enclosure, bracket, or chassis, we select cutting, forming, and joining around your material, thickness, and quantity. The finished-part drawing guides both the first sample and later production batches.
These processes fall into three general categories:
Select laser, punch, waterjet, or etching around thickness, edge quality, and volume.
Control bend order, springback, tool access, and visible-surface marks.
Add joining or hardware, then inspect the interfaces that govern assembly.
Coordinate cutting, bending, stamping, joining, and finishing against one finished-part drawing rather than quoting each operation in isolation.
Order one prototype for fit checks or a small batch for a pilot build. Cutting and bending keep revisions practical before production tooling is needed.
Review bend sequence, hole proximity, grain direction, and burr orientation while the flat pattern can still change.
Define first-article and lot checks around mating features, finish zones, and the surfaces that must remain visible or conductive.

Send CAD files, material, thickness, finish, and quantity for pricing and lead-time review.
Get a Sheet Metal QuoteInitiate your project with instant analysis.
Secure real-time pricing and expert design-for-manufacturing feedback.
Verify specifications to authorize manufacturing.
Precision-crafted parts cleared for delivery.
Laser cutting uses a focused beam around 0.001 in (0.025 mm) in diameter to deliver clean edges and tight profile accuracy for sheet metal parts.
With focal lengths between 1.5 in and 3 in (38-76 mm), this process can hold tolerances near +/-0.002 in (+/-0.05 mm) and kerf widths around 0.006-0.015 in (0.15-0.38 mm), making it suitable for detailed geometry.
Advantages: High precision, minimal finishing, and broad material compatibility.
Get a Sheet Metal Quote
Water jet cutting applies a high-pressure stream, with abrasive when needed, to process thicker materials while preserving edge integrity.
Because it is a cold-cutting method with no heat-affected zone, it is well suited for alloys sensitive to thermal distortion and for parts that require stable material properties after cutting.
Advantages: No thermal damage, high precision, and strong material flexibility.
Get a Sheet Metal Quote
Plasma cutting uses a high-temperature ionized arc to remove material rapidly and cost-effectively, especially on thicker sheet and plate applications.
This method supports high throughput and practical tolerance control for structural components where speed and process economy are top priorities.
Advantages: High cutting speed, lower operating cost, and strong thick-metal capability.
Get a Sheet Metal Quote
Punching forms holes and cutouts by driving a punch through sheet stock into a matching die, creating repeatable features with efficient cycle times.
It is effective for repeated patterns and perforated layouts, and performs best when the feature diameter is appropriately larger than material thickness.
Advantages: Fast production, economical tooling, and repeatable perforation quality.
Get a Sheet Metal Quote
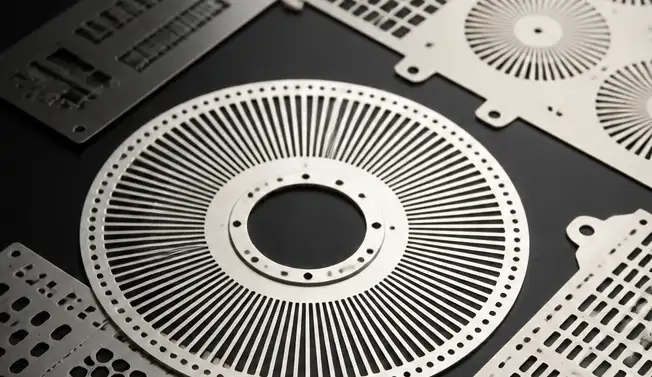
Chemical etching removes metal through a controlled mask-and-etch process instead of mechanical force, making it useful for thin decorative and functional sheet details.
It is a good fit for fine speaker grilles, anti-insect screens, filter meshes, nameplates, logo plates, and textured metal surfaces where clean openings and low burr risk matter.
For automotive trim or consumer hardware, etching can be combined with brushing, plating, painting, or PVD-style finishing when the part needs both pattern accuracy and a controlled surface look.
Advantages: Fine pattern control, low tooling pressure, low burr risk, and strong fit for thin metal details.
Get a Sheet Metal Quote
Some sheet metal parts do not need a heavier forming route. For thin stainless steel or aluminum details, etching can produce repeatable openings, textures, and branding features while keeping the part flat and clean.

Fine openings and repeated graphic details can be controlled without the stress that punching can add to delicate sheet stock.
Etched parts can move into brushing, plating, painting, or other visible finishes when the part sits on an interior or exterior surface.
Open area, airflow, filtration, and sound passage can be reviewed together instead of treating the mesh as only a cosmetic insert.
2D/3D measurement, color review, salt spray, hardness, and visual checks can be added when the program needs documented acceptance.
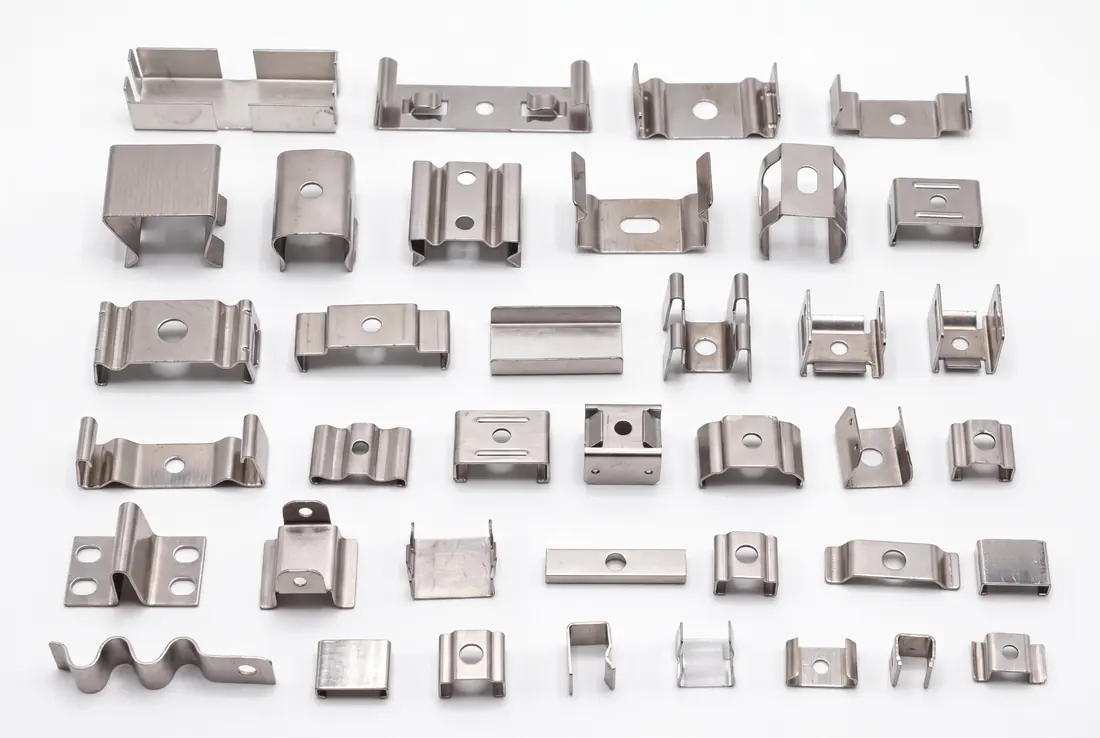
Sheet metal bending forms V, U, and channel profiles using a press brake with controlled force and angle targets based on material thickness and strength.
Because elastic recovery can change final geometry, we apply over-bend compensation for springback so finished parts match drawing intent more consistently.
Bending is widely used for enclosures, brackets, and structural sheet components that require repeatable angular accuracy.
Advantages: Cost-efficient forming, high repeatability, and compatibility with various metals.
Get a Sheet Metal Quote
Production stamping can combine blanking, piercing, and forming in dedicated tooling when the geometry and demand justify a repeat route.
Before tool release, review strip layout, material yield, pilot position, clearance, springback, and scrap removal around the critical features.
First-article approval, in-process sampling, and die maintenance help keep later batches aligned with the validated drawing.
Advantages: Short cycle time after tooling validation, repeatable features, and defined lot-control points.
Get a Sheet Metal Quote
Spinning forms hollow and rotationally symmetric parts by rotating a metal blank on a lathe and progressively pressing it against a shaped tool.
The process can be manual or mechanically assisted depending on geometry complexity and output requirements.
It is commonly selected for cones, hemispheres, and cylindrical forms where smooth surfaces and stable symmetry are required.
Advantages: Smooth finishes, lower tooling cost, and strong fit for rounded geometries.
Get a Sheet Metal Quote
Assembly is the final stage of sheet metal fabrication where multiple parts are combined into a complete functional product.
After cutting, forming, and surface preparation, components are joined with fasteners, rivets, welds, or other standard methods based on performance and service requirements.
We support manual and automated assembly planning for multi-part sheet metal structures, with the joining method matched to the drawing and order quantity.
Advantages: Product readiness, design flexibility, and support for manual or automated methods.
Get a Sheet Metal Quote
Welding fuses sheet metal components through controlled heat input to create strong and permanent joints for structural and enclosure applications.
Materials such as aluminum and stainless steel can be joined through TIG, MIG, or spot welding depending on thickness, joint geometry, and quality targets.
This process is typically scheduled after forming and before final finishing to preserve structural integrity throughout downstream operations.
Advantages: Strong joints, permanent bonding, and compatibility with multiple metals.
Get a Sheet Metal Quote
Choosing the right manufacturing method is key to achieving target part quality. Not sure which method best fits your program?
Contact UsLaser-cut or punched blanks and press-brake forming let teams validate fit, surface appearance, and assembly details before committing to dedicated tooling.
Learn MoreProduce small batches with laser cutting and bending while demand develops. When the drawing and volume stabilize, compare stamping tooling and unit cost for repeat production.
Learn MoreUse these values as early design checks, then confirm bend radii, feature spacing, and tolerances for the actual alloy, thickness, grain direction, and tooling.
| Feature | Recommended Value (MT = Material Thickness) | Notes |
|---|---|---|
| Minimum Bend Radius | 1 x MT | Avoid cracking (may vary by material: soft aluminum <= 0.5 x MT, stainless steel >= 2 x MT). |
| Hole-to-Edge Distance | 2 x MT | Prevents edge deformation during punching. |
| Hole-to-Hole Distance | 6 x MT | Ensures structural integrity (increase for dense hole patterns). |
| Bend-to-Hole Distance | 6 x MT | Prevents hole distortion during bending. |
| Feature-to-Countersink Distance | 8 x MT | Maintains material strength around countersinks. |
| Minimum Countersink Depth | 0.6 x MT | Ensures flush fastener seating (adjust for screw head angle). |
| Relief Cut Width | 1 x MT | Reduces stress concentration at bends (required for sharp corners). |
| Corner Fillet Radius | 0.5 x MT | Improves manufacturability and stress distribution. |
The feedback during quoting helped us fix a problem before release rather than after samples. That saved time we really did not have in the program.
Ora teniamo Zigitech tra i fornitori ogni volta che un programma richiede revisione rapida, comunicazione chiara e consegne affidabili all'estero. Sono stati costanti su diversi ordini.
Vi bestilte aluminiums manifolder til en pilotproduksjon og fulgte tetningsflatene nøye. Delene kom godt pakket og klarte inngående kontroll uten anmerkninger.
What stood out was that the quote review connected design choices to production reality. Our team got clear notes on wall thickness, access, and finish instead of vague suggestions.
Pro program rozvaděčů odpovídaly osazení kování a detaily ohnutí schválené výkresové sadě bez překvapení. Ušetřilo to přepracování na naší montážní straně.
We asked for a tooling review before final approval and got specific comments on shutoffs and cosmetic risk. It felt like feedback from people who actually build these parts.
The turned shaft parts were consistent from sample to sample, which mattered because we were checking fit against bearings and seals. That repeatability is hard to fake.
Mielismy jedno pytanie dotyczące materiału w trakcie zamówienia i otrzymaliśmy prostą odpowiedź z opcjami, a nie opóźnioną odpowiedź sprzedażową. To pomogło nam utrzymać ruch w wewnętrznych akceptacjach.
프로토타입 커버는 고객 데모용으로 보여주기 충분할 만큼 깔끔했고, 동시에 실제 핏 확인에도 사용할 수 있었습니다. 그 단계에서 우리가 딱 필요로 했던 균형이었습니다.
Across a mixed order of parts and jigs, revision control stayed clear all the way through. That made our own internal tracking much easier when the shipment landed.
All information and uploads are secure and confidential.
Upload
Quote
Confirm
Ship
Supports:
We use cookies and similar technologies to enhance your experience, analyze traffic, and for marketing purposes. By clicking "Accept All," you consent to our use of cookies and the processing of your data in accordance with our Privacy Policy